OEE stands for Overall Equipment Effectiveness. Most manufacturing plants run the OEE calculation formula every week, yet very few trust the number it produces. A plant hitting 85% OEE is running at what the industry calls world class, a benchmark that traces back to the original Total Productive Maintenance research, while a typical plant sits closer to 60%, and only about 6% of plants in one 2024 dataset reached the 85% line.
- Why does your OEE number change depending on whether the operator or the supervisor calculates it?
- Where is your line actually losing points: Availability, Performance, or Quality?
- Could you defend your OEE calculation formula if an OEM auditor asked how you arrived at it?
This guide breaks down the OEE calculation formula the way your shop floor actually produces the numbers. We walk through Availability, Performance, and Quality one at a time, then run a full worked example using numbers a Tier 2 auto component line would recognise. By the end, you will know where your plant's OEE calculation formula is really losing points.
TL;DR
|
· The OEE calculation formula is Availability × Performance × Quality, and each factor needs its own accurate input data to mean anything. · Manual, Excel-based OEE calculation usually breaks down at Performance, not Availability, because Ideal Cycle Time is rarely written down correctly. · Knowing which factor drags your score down matters more than the final OEE number itself. · A worked example from an auto component line shows exactly where lost points hide, once one shift is checked factor by factor. · When one shift produces two different OEE numbers from two people, the formula was never the problem. The data feeding it was. |
What Is the OEE Calculation Formula?
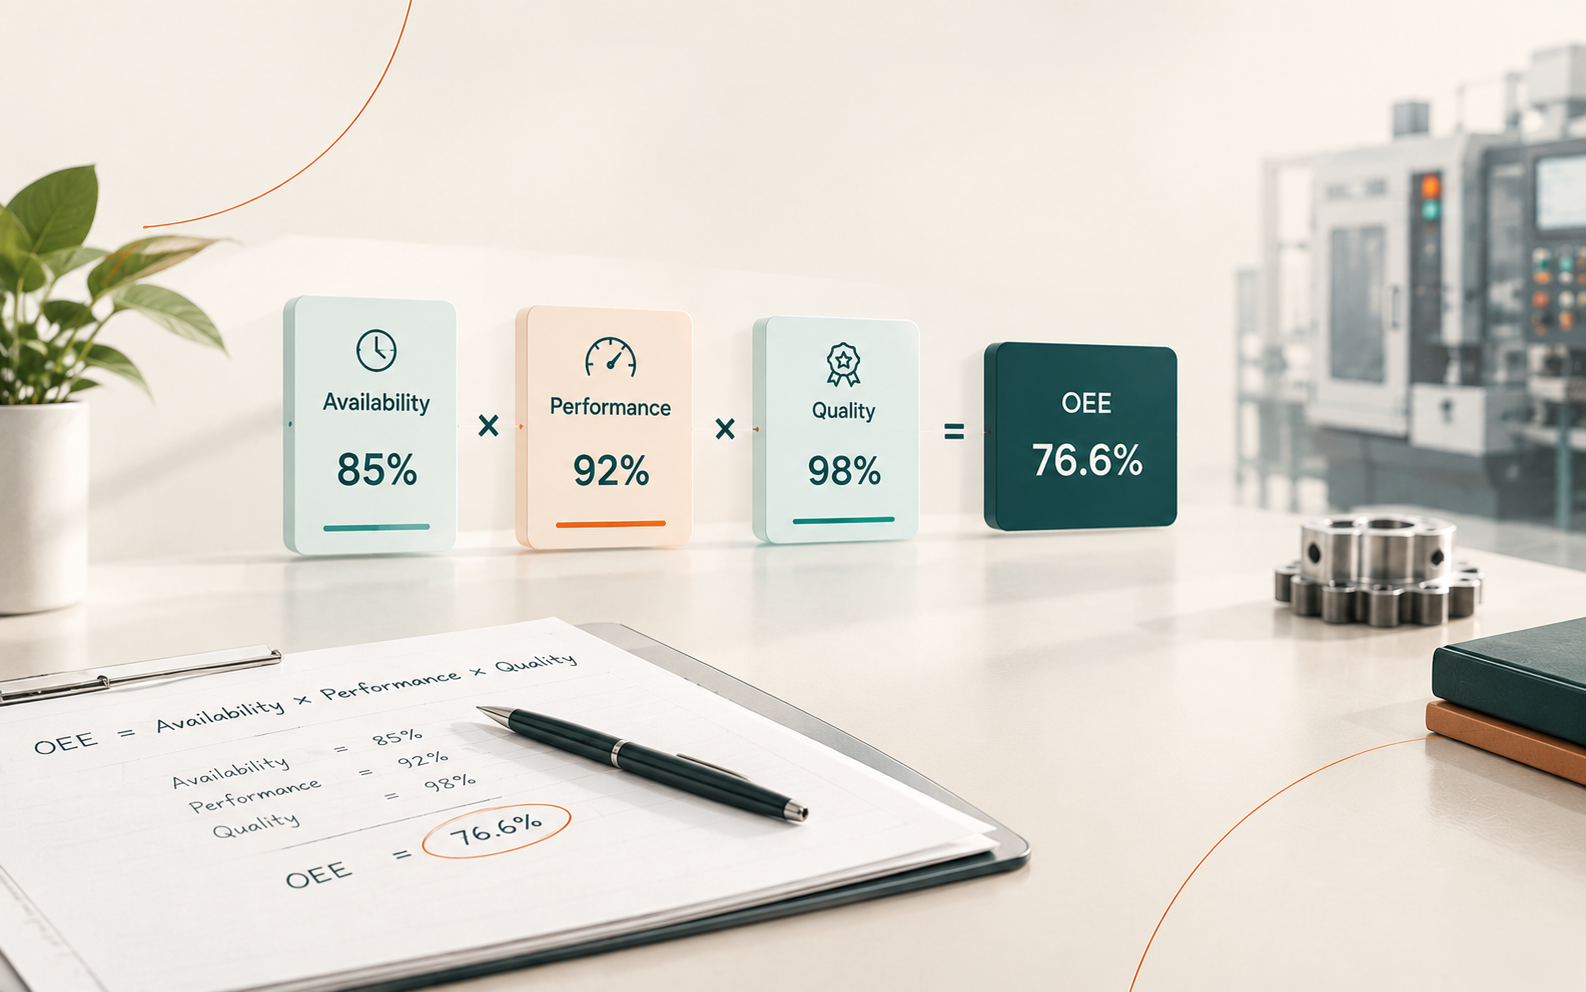
The OEE calculation formula measures how well a machine, or an entire line, turns planned production time into good parts. It multiplies three numbers together: Availability, Performance, and Quality. Each one is a percentage, so the final OEE score is also a percentage.
|
OEE = Availability × Performance × Quality |
This single line looks simple, but it hides three separate data collection problems. Get any one of the three inputs wrong, and the final number stops meaning anything on the floor.
The formula works because it isolates three different kinds of loss. This resulted in:
- Availability loss, from breakdowns, changeovers, and material waits.
- Performance loss, from running slower than the ideal cycle time, or from short stops.
- Quality loss, from parts that need rework or get scrapped.
Knowing the formula is one thing. Calculating each part correctly, using numbers your own shift actually produces, is where most plants lose confidence in it. The next section breaks down exactly how each part is calculated.
How to Calculate Each Part of the OEE Formula
Each part of the OEE calculation formula answers a different question about your shift. Availability asks how much of your planned time the machine actually ran. Performance asks how fast it ran against its rated speed, and Quality asks how many parts it made were good on the first try.
All three numbers come from different registers: the downtime log, the piece counter, and the inspection sheet. When these sources do not talk to each other, the OEE calculation formula becomes a guess dressed up as a percentage.
Availability
|
Availability = Run Time / Planned Production Time |
Run Time is Planned Production Time minus every stoppage, whether it is a breakdown, a changeover, or waiting on material. We have broken down how to log that downtime accurately, reason by reason, in our guide to tracking machine downtime, so we will not repeat it here.
Performance
|
Performance = (Ideal Cycle Time × Total Count) / Run Time |
Ideal Cycle Time is the fastest time your line can safely make one part, not the time it happened to run yesterday. Most manual OEE calculations get this number wrong, because operators round it or pull it from memory instead of the machine's rated spec.
Quality
|
Quality = Good Count / Total Count |
A part only counts as good if it passes on the first try, without rework or scrap. This is usually the most accurate number on the shop floor, because inspection sheets rarely get skipped, even when downtime logs do.
Three formulas, three different data sources, one final score. The real test comes when you run all three together on one shift's numbers, which is exactly what the next section does.
Is your quality data ready for an audit or scattered across notebooks?
Tell us what your plant records look like today. We'll show you what the digital version looks like mapped to your process, not a template.
A Step-by-Step OEE Calculation Example for an Auto Component Line
Numbers make more sense with a real shift behind them. Take a Tier 2 auto component line running an 8-hour shift and making a single machined part. Here is how the OEE calculation formula plays out, step by step.
The key steps involved are:

That single shift now has a real OEE calculation formula behind it, not a guess. It sits below world class, but well within reach of it, as the next section shows. The bigger question is where exactly those lost points are hiding, and that is rarely where plants expect.
Where Your Plant's OEE Number Actually Stands
A single OEE score means little without something to measure it against. Where a plant sits compared to the world class benchmark tells a plant head far more than the number alone. The chart below places our worked example line against the two benchmarks that matter most.

Sitting close to that line is not a failure. It shows real room before the world class mark, and real distance above the typical plant average. What the score alone cannot tell you is which of the three factors is actually holding it back.
That answer rarely matches what the shop floor assumes, and it is worth checking before you spend money fixing the wrong thing.
Why the Same OEE Calculation Gives Three Different Numbers on Your Floor
Ask three people on the same shift to calculate OEE, and you will often get three different answers. The formula never changes, but what each person counts as downtime, or as a good part, usually does.
This is not a training problem. It is a data problem, and it shows up most often in the Performance factor, not Availability as most plants assume.
|
"Performance was the largest OEE gap in the production data Godlan analyzed." Godlan, OEE Availability, Performance and Quality analysis, 2026 Performance gap: 14.5 points below target. Availability gap: 11.2 points. Quality gap: 1.2 points. |

Performance leaks because Ideal Cycle Time rarely lives anywhere near the shop floor. Operators round it, supervisors estimate it, and by the time it reaches a spreadsheet, the number bears little resemblance to the machine's rated speed. Multiply that error across a month of shifts, and your OEE calculation formula stops being a measurement and becomes a rough opinion.
Fixing this is not about training people to calculate better. It is about removing the manual step where the error gets introduced in the first place, which is exactly where the next comparison starts.
OEE Calculation Formula vs Real-Time OEE Tracking
The OEE calculation formula itself never changes, whether you run it by hand or through a system. What changes is where the three inputs come from, and how many hands touch them before they become a percentage.
We have seen plants move from paper to screen before, and the shift is rarely about the math. It is about who enters the number, and when. We covered that shift in what shop floor digitization actually means, and the tracking side in our production tracking software guide, so this section stays on OEE.
|
What changes |
Manual OEE calculation |
Real-time OEE tracking |
|
Downtime source |
Operator memory, end of shift |
Machine signal or barcode scan, logged live |
|
Ideal Cycle Time |
Estimated or copied from an old sheet |
Set once per part, applied every shift |
|
Good count vs scrap |
Counted by hand on the inspection sheet |
Linked to the inspection record automatically |
|
When you see the number |
Next morning, if at all |
During the shift, while it can still be fixed |
|
Who can defend it in an audit |
Whoever remembers how it was calculated |
The system, with a timestamped record |
None of this replaces the OEE calculation formula. It just removes the guesswork sitting between the shop floor and the number your MD sees. That is the exact gap we build for, one line at a time.
Is your quality data ready for an audit or scattered across notebooks?
Tell us what your plant records look like today. We'll show you what the digital version looks like mapped to your process, not a template.
Why Should You Choose Edhaas Digisoft for OEE Tracking?
Auto component plants do not need another dashboard that repeats what Excel already shows. They need the OEE calculation formula fed by numbers that were correct the moment they were recorded, not corrected the next morning.
We build that data layer around your existing shift structure, as part of our production management systems, not the other way around. Run Time, downtime reason, piece counts, and inspection results come from the floor as they happen, so Availability, Performance, and Quality calculate themselves.
What this looks like on your line:
- Downtime logging tied to reason codes, entered at the machine, not reconstructed at shift end.
- Ideal Cycle Time set once per part number, so Performance never depends on memory.
- Inspection results linked automatically, so Quality reflects what QA actually found.
- One OEE number, visible to the plant head and the MD, calculated the same way every time, with numbers on a management dashboard.
One of our manufacturing clients replaced paper production logs with this kind of setup. Production cycle time improved by 40% and reporting delays dropped to zero, because the numbers no longer waited for someone to write them down (see the production dashboard case study).
|
Your OEE calculation formula was never the problem. The gap was always in how the numbers reached it. Schedule a Consultation and we will show you where your line's Performance number is hiding. |
Conclusion
The OEE calculation formula is simple to write down and hard to trust when three different people feed it three different numbers. Most of that gap sits in Performance, not Availability, and it starts long before anyone opens a spreadsheet.
Fix where the number comes from, and the formula finally tells the truth: faster reporting, one defensible number for every audit, and a Performance figure that matches the machine's real speed. That is the difference between calculating OEE once a week and knowing it every shift.
Questions